Designing Out the Blowtorch: Hot Works, Fire Risk and the Case for Press-Fit Jointing
7 September 2026

Today every soldered pipe joint on a construction site comes with a significant amount of administration and risk associated with it. Since the 10th edition of the Fire Prevention on Construction Sites – Joint Code of Practice has been published in August 2023, a dedicated person is supposed to monitor hot work continuously throughout its duration, conduct fire watches for at least one hour after the work is finished and inspect every hour with interval no more than twenty minutes — everything within ten meters, inclusive of adjacent spaces and lower floors. Thermographic cameras are supposed to be applied routinely, before, during and after hot work.
Non-conformity with the code could result in loss of insurance coverage, contract termination and, in extreme cases, even prosecution.
Insurance company loss prevention guidelines about hot works are much more straightforward. According to Munich Re’s HSB guide to hot work fires, the ideal scenario would be that no hot works are performed at all and other options are considered prior to that. In case these other options have been tried and are no longer feasible, then hot work is permitted by formal permit — only for one particular task, in one particular place, by one particular person, once per day shift.
All this changes the context dramatically for anyone who specifies or coordinates building services. How pipes are joint together is no longer simply the matter for installers to decide. That choice impacts fire risk, schedule, insurance policy and even occupancy status of the building while work progresses.
What is press-fit jointing?
Short answer: Press-fit is the mechanical way of joining metallic pipes. Fitting with elastomeric seal is pressed to prepared end of a pipe and deformed by means of a powered tool with profile jaws in one press-cycle, typically lasting several seconds. The result is a permanently sealed mechanical joint without using fire, flux or solder.
The press cycle is short and highly repetitive – square-cut the pipe, deburr and clean the end, insert to the appropriate mark, install the appropriate jaws for the size pipe, square the tool to the fitting, and press. The process is described in much greater detail, with all relevant tooling and jaw details covered in this guide to press fittings installation.
Two aspects are significant with regard to safety. Almost every system uses the concept of leak before press, meaning that an unpressed fitting is clearly visible and audible during system testing, rather than hidden behind a wall – the single most common concern about press-fitting ever raised and largely addressed by design. Many also include a frangible indicator ring that breaks off after the press is complete, creating a visible record of the completed connections.
Press fittings used for metal tube come under the EN 1254 standard, and are available in copper, stainless steel and carbon steel across a wide range of diameters, from tiny domestic plumbing through to heavy commercial piping.

Where this changes the specification conversation
Short answer: Pressing is most important in situations where there is a difficulty, expense, or prohibition on open flames – in other words, increasingly, refurbishments, occupied buildings, historic fabric and any project on which the fire watch requirement would be critical path.
Occupied buildings. Hospitals, nursing homes, laboratories, schools, hotels and working office space are all clear cases. Flameless joining avoids the permit-and-fire-watch process chain for every stage of services changeover, and actually makes phased work in occupied premises possible rather than theoretically possible.
Heritage and timber frame structure. In listed buildings and any historic roof structures and any environment containing hidden timber structures, insulation or void space, the risk assessment for hot works is critical, and the consequences of doing it incorrectly are irreparable. Both conservation officers and insurers prefer a solution that eliminates the ignition source completely.
Programme and sequencing. Fire watch is not merely a formal exercise; it is at least two hours of monitored time per each hot works session, the permit documentation management, and the labour of the fire watcher. In case of installation of a significant number of joints in the services system (hundreds of joints), elimination of this chain will have a considerable effect on the programme.
Offsite and modular construction. Services systems prefabrication and MMC construction require fast and efficient jointing. Torch works do not suit factory environments and repeatable quality assurance.
Information trail. With a higher risk building, where regulations demand traceability of the specification and construction process, the solution with a visible completion indicator and clear process is preferable to the solution, quality of which depends on the individual doing the hot works.
What architects need to allow for on the drawing
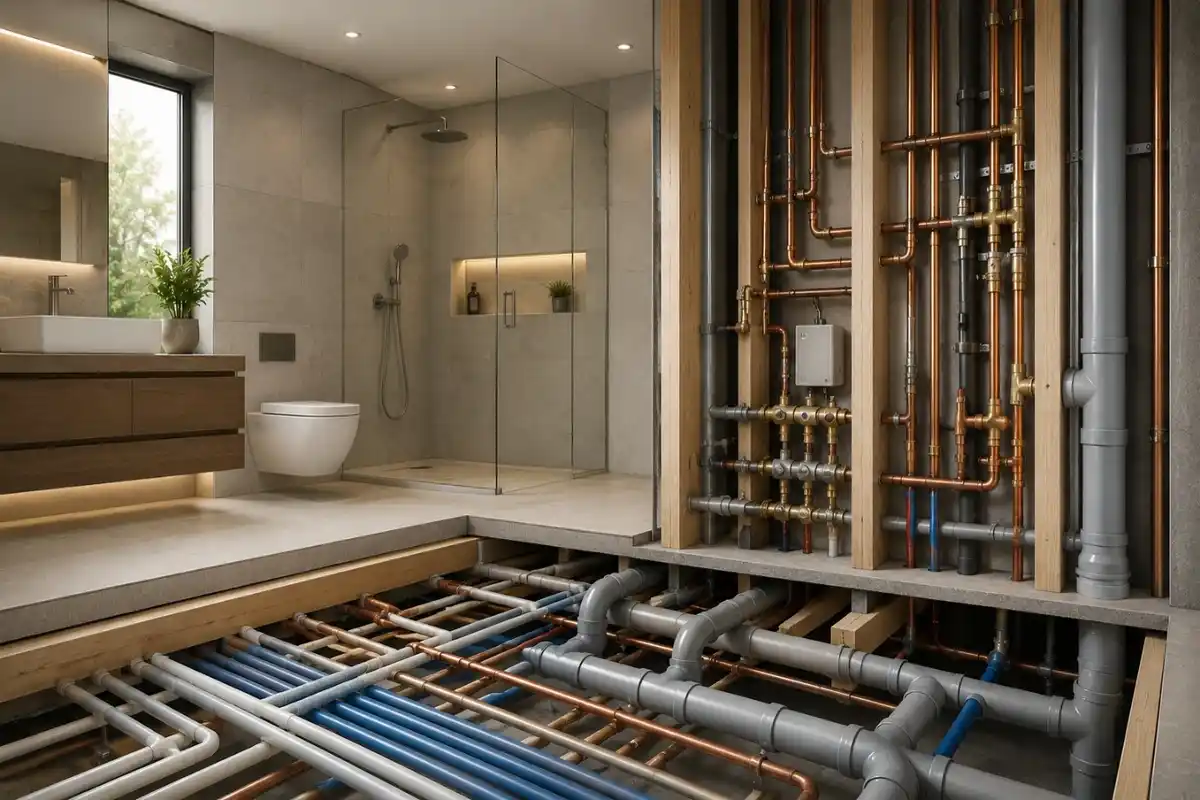
It is when press fit stops being a contractor’s responsibility and becomes an issue of coordination, because the method has certain requirements for the space that torch works lack.
Clearance. An open-jaw press fitting takes up significantly more volume compared to the blowtorched version in one’s hand. Jaws have to seat perpendicular to the fitting, and the tool housing requires extra space behind them. A joint tightened into the corner of a duct, jammed against the slab soffit or located in the middle of an obstructed riser may be unobtainable physically. Tool head rotation helps, but does not remove the requirement.
Access and maintenance voids. Voids in the ceiling, width of risers, clearances in plant rooms and access panels have to account for the size of the pressing equipment as well, including the maintenance aspect, as no joint can be remade if it is unaccessible for pressing tools.
System uniformity. Press systems are not universally compatible. Fittings and jaws profiles are coordinated by the manufacturer, and combining systems in one installation leads to incompatible joints. The specifications have to define the press system, not just the press-fit fittings.Selection of sealing element. The material of the sealing ring has to correspond to the medium and temperature: rubber compounds suitable for potable water, heating circuits, gas and high temperature media are different and usually color-coded to allow easy identification. This is the specification item that can not be left unattended by the designer. Appropriate press-fits and sealing elements have to be checked against the manufacturer’s data.
The honest limitations
The professional audience has a right for the opposite point of view, and there is such a point of view.
Press tooling is a genuine cost and genuine dependency. Press tools are expensive to purchase, need calibration and servicing, typically on average about 10,000 press cycles apart, and a press tool that needs to be calibrated is a systemically defective one and not just a sporadically defective one. With a smaller project, the up-front costs may never be recovered.
Press components are also more expensive. Fittings for presses cost more per piece than fittings for soldering. The cost is in labour, programming and risk, and not material, and the argument is least valid in projects with few connections and with no hot work restriction.
It is not a stand-in for competence. Proper insertion, square cutting, thorough deburring and proper jaw seating are all important, and while the failure mechanisms are different from soldering, they are not fewer. Leak before press detects the improperly pressed joint, but will not detect an improperly seated seal or a poorly prepared pipe end.
There are applications where it cannot be used. Medium, temperature, pressure and material of the pipe limit its applicability, and there are some projects where another type of connection will be the right way.
None of these negate the core of the argument. It does mean press fit needs to be selected explicitly for a good reason and not because it was the default one.
A short checklist for specifiers
- Considerations for hot works limitations must be determined early – occupied, historic, timber frame or high risk building fabric must raise the question from concept, not tender
- State the system, not just the method, and prevent mixing manufacturers’ fixtures and jaws
- Determine sealing element material compatibility with the medium and design temperature for each service
- Assess clearance for tools at congested joints, risers and ceiling voids during coordination, not at the construction phase
- Plan for future maintenance access, because rebuilding the joint requires the same clearance as constructing the joint
- Where the information requirements of the project dictate, document the decision and reasoning behind it
FAQ
What are press fittings? Fittings comprising a sealing ring made of elastomer which is permanently formed around a prepared end of pipe using power-driven press tooling without the use of flame, flux or solder. Metal tube press fittings have EN 1254 range of standards.
Why are press fittings preferred over soldering? In order to avoid hot work which, according to the 10th edition of Joint Code of Practice, necessitates a hot work permit, supervision throughout, fire watching for at least an hour after and another hourly inspection thereafter.
Are press fittings acceptable for commercial and public buildings? Yes, and this is when the case is most compelling. Hospitals, schools, laboratories, hotels and offices get the greatest advantage since the works can be done without any risk of fire nor require permits in a live building.
What is leak before press? Leak before press is a design approach by which the joint will be leaking visibly during system testing instead of being apparently sealed. This solves the age-old problem of potentially undetected miss-pressing behind finished construction.
What should be considered by architects when press fittings are specified? Consideration should be made regarding physical space for the press tool jaws at each joint, the dimensions of risers and ceilings, the need for access for maintenance purposes, and specifying one particular system instead of press fittings in general.
Is the cost of using press-fit assemblies higher than that of using soldered joints? Yes, per fitting; but the cost of the tooling equipment is substantial. The economics are based on speed, programme, and the absence of risk of hot works, not on cost of material.
References: Fire Prevention at Construction Sites – Joint Code of Practice, 10th Edition (August 2023); Munich Re HSB, “Fire due to Hot Work – Loss Prevention Guide”; EN 1254 series.
Comments on this guide to Hot works, fire risk and press-fit jointing article are welcome.
Building
Recently added Building posts
Plan7Architect Pro – Put to the Test by Professional Architects
Subterranean garage construction
+++
Property
Residential Property Design
Comments / photos for the Hot works, fire risk and press-fit jointing advice guide page welcome.